
Introduction to Empty Capsules
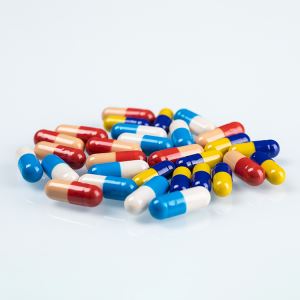
Empty capsules are an essential component in the pharmaceutical and nutraceutical industries. They serve as a convenient and reliable way to encapsulate various substances, including powders, granules, and liquids. These capsules provide a protective barrier for the contents, preventing them from being affected by external factors such as moisture, light, and air. They also offer a standardized dosage form, making it easier for consumers to take the right amount of the active ingredients.
Empty capsules are typically made from materials such as gelatin, hydroxypropyl methylcellulose (HPMC), or other plant - based polymers. Gelatin capsules are derived from animal sources and are known for their excellent solubility and compatibility with a wide range of substances. HPMC capsules, on the other hand, are vegetarian and vegan - friendly, making them a popular choice for consumers with specific dietary preferences.
Top 10 Empty Capsule Factories
1. Zhejiang Tianlong Capsule Co., Ltd.
Zhejiang Tianlong Capsule Co., Ltd. is a leading manufacturer of empty capsules in China. With years of experience in the industry, the company has established a strong reputation for producing high - quality capsules. It is committed to strict quality control measures throughout the production process, from raw material selection to the final product inspection.
The company offers a wide range of capsule products, including gelatin capsules and HPMC capsules. These capsules are available in various sizes and colors to meet the diverse needs of customers in the pharmaceutical, nutraceutical, and cosmetic industries.
Features in Empty Capsule Production:
- Advanced Technology: Zhejiang Tianlong Capsule Co., Ltd. uses state - of - the - art production technology. Their automated production lines ensure high - precision manufacturing, resulting in capsules with consistent wall thickness and excellent sealing performance.
- Customization: The company can customize capsules according to customers' specific requirements. Whether it is a special size, color, or print on the capsule, they have the ability to meet these demands.
- Quality Assurance: They have a comprehensive quality management system. All raw materials are carefully tested for purity and quality, and the final products are also subject to multiple quality checks to ensure compliance with international standards.
Advantages:
- Cost - effectiveness: By optimizing their production processes and supply chain management, the company can offer competitive prices without sacrificing quality.
- Large - scale Production Capacity: With large - scale production facilities, they can meet large - volume orders in a timely manner, which is crucial for pharmaceutical and nutraceutical companies with high - demand products.
- Good Reputation: Their long - standing presence in the market and positive customer feedback have built a good reputation, which gives customers confidence in their products.
Website: https://www.tlcapsules.com/
2. Capsugel (now part of Lonza)
Capsugel has a long - standing history in the empty capsule manufacturing industry. It was one of the pioneers in developing innovative capsule technologies. After being acquired by Lonza, it has further strengthened its position in the global market.
Capsugel offers a diverse portfolio of capsule products. Their Vcaps Plus HPMC capsules are well - known for their vegetarian - friendly nature and excellent performance in encapsulating a wide range of actives. They also have a line of gelatin capsules that are highly soluble and suitable for both immediate - release and modified - release formulations.
Features in Empty Capsule Production:
- Innovative Formulations: Capsugel has a strong R & D team that is constantly working on developing new capsule formulations. For example, they have developed capsules with enhanced stability for sensitive actives, which can protect the active ingredients from degradation during storage and transportation.
- Global Reach: With manufacturing facilities and distribution networks around the world, they can quickly supply capsules to customers in different regions. This global presence also allows them to understand and adapt to local market needs.
- Regulatory Compliance: They are well - versed in meeting strict regulatory requirements in different countries. Their products comply with international standards such as the United States Pharmacopeia (USP), European Pharmacopoeia (EP), and Japanese Pharmacopoeia (JP).
Advantages:
- Brand Recognition: The Capsugel brand is widely recognized and trusted in the pharmaceutical and nutraceutical industries. This brand reputation gives their customers an edge in the market.
- Technical Expertise: Their long - term experience and in - depth knowledge in capsule technology enable them to provide excellent technical support to their customers. They can assist in formulation development and troubleshooting.
- Diverse Product Range: The wide variety of capsule types and sizes they offer allows customers to find the most suitable capsule for their specific products.
3. Suheung Capsule Co., Ltd.
Suheung Capsule Co., Ltd. is a South Korean company that has made significant contributions to the empty capsule market. It has a modern manufacturing facility equipped with advanced production equipment.
The company produces both gelatin and vegetarian capsules. Their vegetarian capsules are made from high - quality plant - based materials and have good mechanical properties, making them suitable for automatic filling machines.
Features in Empty Capsule Production:
- Quality - focused Manufacturing: Suheung places a high emphasis on quality. They have strict quality control procedures at every stage of production. From the sourcing of raw materials to the final packaging, each step is carefully monitored to ensure the capsules meet the highest quality standards.
- Research and Development: They invest in R & D to improve their capsule products. For instance, they are constantly working on enhancing the dissolution rate of their capsules to improve the bioavailability of the encapsulated actives.
- Sustainable Practices: The company is committed to sustainable manufacturing. They use eco - friendly raw materials and have implemented energy - saving measures in their production facilities.
Advantages:
- Proximity to Asian Markets: Being based in South Korea, it has a geographical advantage in serving the Asian market. They can quickly respond to the needs of Asian pharmaceutical and nutraceutical companies, reducing lead times and transportation costs.
- Good Customer Service: They provide excellent customer service, including prompt response to inquiries, technical support, and after - sales service. This helps build long - term relationships with their customers.
- Continuous Improvement: Their dedication to continuous improvement in product quality and production processes allows them to stay competitive in the global market.
4. ACG Worldwide
ACG Worldwide is a global player in the pharmaceutical packaging and empty capsule manufacturing industry. They have a comprehensive range of products and services related to the pharmaceutical and nutraceutical sectors.
ACG's empty capsules are known for their high - quality construction. Their capsules are designed to be compatible with a wide range of filling machines, ensuring smooth and efficient production processes for their customers.
Features in Empty Capsule Production:
- Integrated Solutions: ACG offers integrated solutions for the pharmaceutical industry. In addition to empty capsules, they also provide filling machines, packaging equipment, and related services. This one - stop - shop approach is convenient for customers as they can get all their needs met from a single provider.
- Quality Control and Traceability: They have a strict quality control system with full traceability of raw materials and production processes. This allows them to quickly identify and address any quality issues, ensuring the safety and efficacy of their capsules.
- Global Technical Support: With a global network of technical support teams, they can provide on - site assistance to their customers. Whether it is installation, maintenance, or troubleshooting of filling machines or capsule - related issues, their teams are readily available.
Advantages:
- Industry Experience: ACG has decades of experience in the pharmaceutical industry. This experience gives them a deep understanding of the industry's requirements and challenges, allowing them to develop products that meet the highest standards.
- Innovation in Packaging: Their expertise in packaging technology also benefits their empty capsule products. They can offer innovative packaging solutions for capsules, such as blister packs with enhanced protection features.
- Strong Financial Position: A strong financial position enables them to invest in new technologies, R & D, and expansion, ensuring their long - term competitiveness in the market.
5. Shionogi Qualicaps Co., Ltd.
Shionogi Qualicaps is a well - respected company in the empty capsule manufacturing field. It has a long - standing reputation for producing high - quality capsules, especially in the Japanese and Asian markets.
The company offers a variety of capsule types, including gelatin and HPMC capsules. Their capsules are known for their smooth surface, which is beneficial for the filling process as it reduces friction and improves the accuracy of filling.
Features in Empty Capsule Production:
- Japanese - style Precision Manufacturing: Shionogi Qualicaps adheres to Japanese manufacturing principles of precision and quality. Their production processes are highly controlled, resulting in capsules with very tight tolerances in terms of size and shape.
- Compatibility with Japanese Standards: Their products are well - suited for the Japanese market, which has strict regulatory requirements. They also meet international standards, making them suitable for global distribution.
- Research on Active Ingredient Compatibility: The company conducts extensive research on the compatibility of their capsules with different active ingredients. This helps ensure that the capsules do not interact negatively with the actives, maintaining the stability and efficacy of the final products.
Advantages:
- Reliability: Their long - term presence in the market and consistent product quality have made them a reliable partner for pharmaceutical and nutraceutical companies.
- Knowledge of Asian Markets: Their in - depth knowledge of Asian markets, including consumer preferences and regulatory environments, gives them an advantage in serving Asian customers.
- Collaboration Opportunities: They often collaborate with research institutions and pharmaceutical companies on new product development, which allows them to stay at the forefront of capsule technology.
6. Lapi Pharma
Lapi Pharma is an Italian company that has been involved in the production of empty capsules for many years. It has a reputation for producing high - quality, innovative capsule products.
The company's capsules are made from high - purity raw materials. They offer a range of sizes and types, including hard gelatin capsules and vegetarian capsules.
Features in Empty Capsule Production:
- Artisanal - like Craftsmanship with Modern Technology: Lapi Pharma combines traditional artisanal craftsmanship with modern production technology. This results in capsules with a unique quality and attention to detail. For example, their capsules have a smooth and uniform appearance, which is aesthetically pleasing.
- Sustainable and Ethical Sourcing: They are committed to sustainable and ethical sourcing of raw materials. They work closely with suppliers to ensure that the materials are obtained in an environmentally friendly and socially responsible manner.
- Product Innovation: Lapi Pharma invests in R & D to develop new capsule products. They have introduced capsules with special coatings for modified - release applications, which can control the release of active ingredients over time.
Advantages:
- European Quality Standards: Their products adhere to strict European quality standards. This gives them an edge in the European market and also makes them attractive to international customers who value high - quality products.
- Customization and Flexibility: They are very flexible in terms of customization. Whether it is a small - batch order with specific requirements or a large - scale production, they can accommodate their customers' needs.
- Cultural Heritage and Reputation: Their long - standing presence in the Italian market and their cultural heritage associated with high - quality manufacturing give them a unique selling point in the global market.
7. CapsCanada Corporation
CapsCanada is a leading empty capsule manufacturer in North America. It has a strong foothold in the North American market and is also expanding its presence globally.
The company's empty capsules are designed to meet the specific needs of the North American pharmaceutical and nutraceutical industries. Their capsules are known for their high - performance in terms of filling and sealing.
Features in Empty Capsule Production:
- North American - specific Design: CapsCanada designs its capsules to be compatible with the filling machines and production processes commonly used in North America. This ensures seamless integration into the local production lines of its customers.
- Quality Assurance for North American Regulations: They are well - versed in meeting the strict regulatory requirements of the United States and Canada. Their quality control systems are designed to comply with regulations such as the FDA's Good Manufacturing Practices (GMP).
- Customer - centric Approach: The company focuses on understanding its customers' needs. They offer personalized services, such as customized capsule design and packaging, to meet the unique requirements of different customers.
Advantages:
- Local Market Knowledge: Their in - depth knowledge of the North American market allows them to quickly respond to market trends and customer demands. This gives them an advantage over international competitors in serving the local market.
- Proximity to Raw Material Sources: Being located in North America, they have access to high - quality raw materials from local sources. This can reduce transportation costs and lead times, as well as ensure the freshness and quality of the raw materials.
- Good Industry Network: CapsCanada has a strong network within the North American pharmaceutical and nutraceutical industries. This network helps them in terms of marketing, collaboration, and staying updated on the latest industry developments.
8. Caps India Limited
Caps India Limited is a prominent player in the Indian empty capsule market and is also making its mark on the global stage.
The company produces a wide range of empty capsules, including both gelatin and vegetarian capsules. Their capsules are known for their cost - effectiveness and good quality.
Features in Empty Capsule Production:
- Cost - effective Manufacturing: Caps India Limited has optimized its production processes to achieve cost - effective manufacturing. They use local raw materials and efficient production techniques, which allows them to offer competitive prices without compromising on quality.
- Adaptability to Indian Market Conditions: They understand the unique market conditions in India, such as the diverse range of customer needs and the price - sensitive nature of the market. Their products are designed to meet these specific requirements.
- Export - oriented Production: With an eye on the global market, they have established production processes that meet international quality standards. This enables them to export their capsules to various countries around the world.
Advantages:
- Large - scale Production in India: India's large - scale manufacturing capabilities give Caps India Limited the ability to produce a large volume of capsules at a relatively low cost. This is beneficial for both domestic and international customers looking for cost - effective solutions.
- Skilled Labor Force: India has a large pool of skilled labor in the manufacturing sector. Caps India Limited can leverage this skilled workforce to ensure high - quality production and efficient operations.
- Growing Global Presence: As the company continues to expand its export business, its global presence is growing. This allows them to access new markets and customers, further strengthening their position in the global empty capsule industry.
9. Capsuline (a division of Rafa Laboratories)
Capsuline is a well - known name in the empty capsule manufacturing industry. It is part of Rafa Laboratories, which gives it access to additional resources and expertise in the pharmaceutical field.
Capsuline's empty capsules are characterized by their high - quality materials and precise manufacturing. Their capsules are suitable for a wide range of applications, from pharmaceuticals to nutraceuticals.
Features in Empty Capsule Production:
- Pharmaceutical - grade Quality: Capsuline adheres to strict pharmaceutical - grade quality standards. Their capsules are manufactured in cleanroom environments to prevent contamination and ensure the safety and efficacy of the encapsulated actives.
- Research - driven Development: They invest in research to develop new and improved capsule products. For example, they are working on capsules with enhanced bioavailability features, which can improve the absorption of active ingredients in the body.
- Quality Control at Every Step: From raw material inspection to final product testing, Capsuline has a comprehensive quality control system. This ensures that every capsule meets the highest quality standards.
Advantages:
- Association with Rafa Laboratories: The association with Rafa Laboratories gives Capsuline access to advanced R & D facilities, regulatory expertise, and a wider distribution network. This helps in the development and marketing of its empty capsule products.
- High - quality Reputation: Their reputation for producing high - quality capsules in the pharmaceutical industry gives them a competitive edge. Customers trust their products for the safety and efficacy of their formulations.
- Innovation and Adaptability: Their focus on research and development allows them to quickly adapt to new market trends and customer requirements. They can introduce innovative capsule products to meet the changing needs of the industry.
10. Medisca Inc.
Medisca is a Canadian company that is actively involved in the empty capsule manufacturing business. It has a diverse product portfolio and a strong customer base in the North American and international markets.
Medisca's empty capsules are known for their compatibility with a wide range of active ingredients. Their capsules are designed to protect the actives from degradation and ensure their stability during storage and use.
Features in Empty Capsule Production:
- Compatibility Testing: Medisca conducts extensive compatibility testing of its capsules with different active ingredients. This helps ensure that there are no negative interactions between the capsule and the active, which is crucial for the quality and efficacy of the final product.
- Customized Packaging: They offer customized packaging solutions for their empty capsules. Whether it is blister packs, bottles, or other types of packaging, they can design and produce packaging that meets the specific needs of their customers.
- Quality Assurance for International Markets: Medisca's quality control system is designed to meet international standards. This allows them to export their capsules to various countries around the world, ensuring a consistent level of quality across different markets.
Advantages:
- North American and International Market Reach: With a strong presence in North America and an expanding international market, Medisca can serve a wide range of customers. This geographical diversity helps in risk - sharing and business growth.
- Product Diversification: In addition to empty capsules, Medisca also offers other pharmaceutical and nutraceutical products. This product diversification gives them an advantage in terms of customer retention and cross - selling opportunities.
- Customer - focused Business Model: Their customer - focused business model emphasizes understanding and meeting the needs of their customers. They provide excellent customer service, from product selection to after - sales support.
Summary
The top 10 empty capsule factories in the world in 2025 represent a diverse range of companies from different regions, each with its own unique strengths and features. Zhejiang Tianlong Capsule Co., Ltd. stands out with its cost - effectiveness, customization capabilities, and large - scale production capacity. Capsugel (now part of Lonza) is known for its innovative formulations and global reach. Suheung Capsule Co., Ltd. offers sustainable practices and proximity to Asian markets. ACG Worldwide provides integrated solutions and global technical support. Shionogi Qualicaps is recognized for its Japanese - style precision manufacturing. Lapi Pharma combines artisanal craftsmanship with modern technology. CapsCanada Corporation has a strong foothold in the North American market. Caps India Limited offers cost - effective manufacturing and is expanding globally. Capsuline benefits from its association with Rafa Laboratories and high - quality reputation. Medisca Inc. has a diverse product portfolio and a customer - focused business model.
These companies play a crucial role in the pharmaceutical and nutraceutical industries by providing high - quality empty capsules. Their continuous innovation, focus on quality, and ability to meet the diverse needs of customers will drive the development of the empty capsule market in the future.