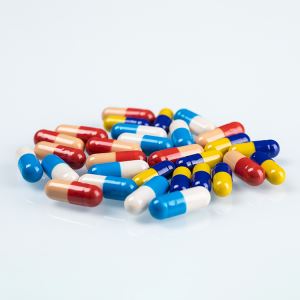

The use of colored pill capsules in the pharmaceutical industry has a long and fascinating history, evolving from simple functional containers to sophisticated tools for branding, patient compliance, and product differentiation. As a colored pill capsule supplier, I am deeply involved in this industry and have witnessed firsthand the significant role these capsules play.
Early Beginnings
The concept of encapsulating medications dates back to ancient times. The Egyptians were among the first to use natural materials to enclose substances for medicinal use. However, the modern - day pill capsule as we know it started to take shape in the 19th century.
In 1834, Mothes and Dublanc in France patented the first gelatin capsule. These early capsules were simple, transparent, and primarily designed to mask the taste and odor of medications. The use of gelatin was a game - changer as it was non - toxic, easy to manufacture, and could be easily digested in the human body.
The Emergence of Colored Capsules
The addition of color to pill capsules came about for several practical reasons. One of the earliest motivations was to distinguish different types of medications. In a pharmacy setting, it was crucial to quickly identify various drugs to prevent errors in dispensing. By adding pigments to the gelatin [1], manufacturers could create visually distinct capsules, reducing the risk of mix - ups.
Another factor was consumer acceptance. Medications often have unpleasant tastes and odors. A colorful capsule made the pills more appealing to patients, especially children. The bright and eye - catching colors could make the process of taking medicine less intimidating, which in turn improved patient compliance.
In the late 19th and early 20th centuries, as the pharmaceutical industry began to grow, the demand for colored capsules increased. Pharmaceutical companies started to explore different color combinations and designs. This was also a period when the regulation of colorants in capsules began. The safety of the pigments used became a primary concern for both manufacturers and regulatory bodies.
Technological Advancements in Coloring
Over time, technology has significantly improved the way colored pill capsules are produced. Early coloring methods involved simply mixing pigments into the gelatin solution. However, this led to issues such as uneven color distribution and fading over time.
Today, we use advanced manufacturing techniques to ensure consistent and long - lasting color. For example, some of the modern methods involve coating the Gelatin Shell [/gelatin - capsule/gelatin - shell.html]. This not only provides a more uniform color but also offers additional protection for the medication inside.
The development of high - quality, food - grade and pharmaceutical - grade colorants has also been a major advancement. These colorants are carefully selected to meet strict safety standards. They are resistant to light, heat, and moisture, ensuring that the color of the capsule remains vibrant throughout its shelf life.
Branding and Marketing with Colored Capsules
In the competitive pharmaceutical market, branding has become a crucial aspect. Colored pill capsules offer an excellent opportunity for pharmaceutical companies to differentiate their products. Just like a logo or a brand name, a unique - colored capsule can become a recognizable symbol of a particular medication.
For example, a well - known pain reliever might always come in a red - and - white capsule. This consistent branding helps consumers easily identify the product on the pharmacy shelf and builds trust over time. Pharmaceutical companies often work closely with capsule suppliers to develop custom - colored capsules that align with their brand identity.
Patient Compliance and Colored Capsules
Patient compliance is a significant issue in the pharmaceutical industry. Many patients find it difficult to adhere to their medication regimens, especially when they have to take multiple medications. Colored capsules can play a role in improving compliance.
For instance, a patient taking three different medications can organize their daily dosage based on the color of the capsules. It becomes easier to remember which pill to take at what time. Some pharmaceutical companies even design capsules with different colors for different days of the week or different stages of treatment. This visual cue can help patients stay on track with their treatment plans.


Current Trends and Future Outlook
Currently, there is a growing trend towards more sustainable and eco - friendly capsule production. As a colored pill capsule supplier, we are constantly researching and developing new materials and processes to reduce our environmental impact.
In addition, the use of smart capsules, which combine the traditional functions of a capsule with new technologies such as sensors and drug delivery systems, is on the rise. These smart capsules may also incorporate color - coding for additional functionality, such as indicating the status of drug release or the progress of treatment.
Looking to the future, we anticipate that colored pill capsules will continue to evolve. They will not only serve as a means of protecting and delivering medications but also as a platform for innovation in patient care and pharmaceutical marketing.
Our Role as a Colored Pill Capsule Supplier
As a supplier in this dynamic industry, we are committed to providing high - quality colored pill capsules. We offer a wide range of colors and styles to meet the diverse needs of our customers. Whether it's a simple single - colored capsule or a multi - colored, branded capsule, we have the expertise and technology to deliver.
Our Empty pill capsule products are made from the finest gelatin materials and are designed to be easily filled with medications. We also provide Fillable Gelatin Capsule options, which offer flexibility for pharmaceutical companies in the drug - filling process.
We understand the importance of quality control and compliance in the pharmaceutical industry. That's why we adhere to strict manufacturing standards and regulations to ensure the safety and effectiveness of our capsules.
Conclusion and Call to Action
The history of using colored pill capsules in the pharmaceutical industry is rich and full of innovation. From their humble beginnings as simple taste - masking tools to their current role in branding, patient compliance, and technological advancement, these capsules have come a long way.
If you are a pharmaceutical company looking for a reliable colored pill capsule supplier, we invite you to engage in a partnership with us. We are ready to discuss your specific requirements, provide samples, and work with you to develop the perfect capsules for your medications. Contact us today to start the conversation and explore how we can help you elevate your pharmaceutical products.
References
[1] Ritschel, W. A., & Kipp, H. (2009). Handbook of Pharmaceutical Controlled Release Technology. Informa Healthcare.